ENABLING AUTONOMOUS MANUFACTURING
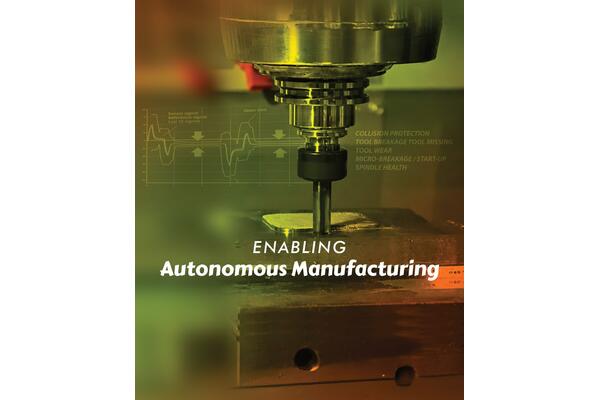
The transition to unmanned manufacturing requires seamless, real-time monitoring of all machining processes. This article explores how the GENIOR MODULAR process monitoring system and GEMCMS collision monitoring system from Marposs (Artis), in combination with the corresponding visualization and analysis software, can support safe and reliable autonomous production.
Rising cost pressures, the shortage of qualified machinists, and the need to utilize expensive machine parks around the clock are forcing the industry toward automation. ‘Lights-Out Manufacturing’ describes the vision of a factory that operates with high productivity during night and weekend shifts without any personnel — with the lights turned off.
However, this autonomy carries a massive risk: if human sensory perception (hearing abnormal machining noises, seeing chip jams, feeling vibrations) is eliminated, the machine tool loses its final safety mechanism. A single undetected tool breakage at the start of an 8-hour unmanned shift can trigger a cascade of scrap production, quality issues or, in the worst case, destroy the main spindle.
Use of Monitoring SystemsUse of Monitoring Systems
The applications of monitoring systems are diverse and span various stages of manufacturing.
- Detection of breakage, missing parts, and wear in machining production
- Machine protection and collision detection
- Prevention of scrap, rework, and consequential damage
- Detection of clamping errors, incorrect components, unbalances and faulty processes
- Condition-based monitoring (CBM) of bearings, ball screws and other machine components
- Adaptive control for increasing machine productivity and overload prevention
- Acquisition and processing of process data
- Process visualization, documentation and reporting
- Energy monitoring of machines and aggregates
- Source of information for other third-party systems
- Data provision for cloud-based systems
- Fulfilling production specifications for aircraft (e.g. P11TF12), energy management (e.g. ISO 50001) and other.
The Technological Nervous System: GENIOR MODULAR & GEMCMS
With the Artis monitoring systems, Marposs offers a market-leading solution specifically developed to address the challenges mentioned above. The system consists of the core components: sensors, measurement converters, and a main unit. The visualization opens a window to the machining process.
GENIOR MODULAR
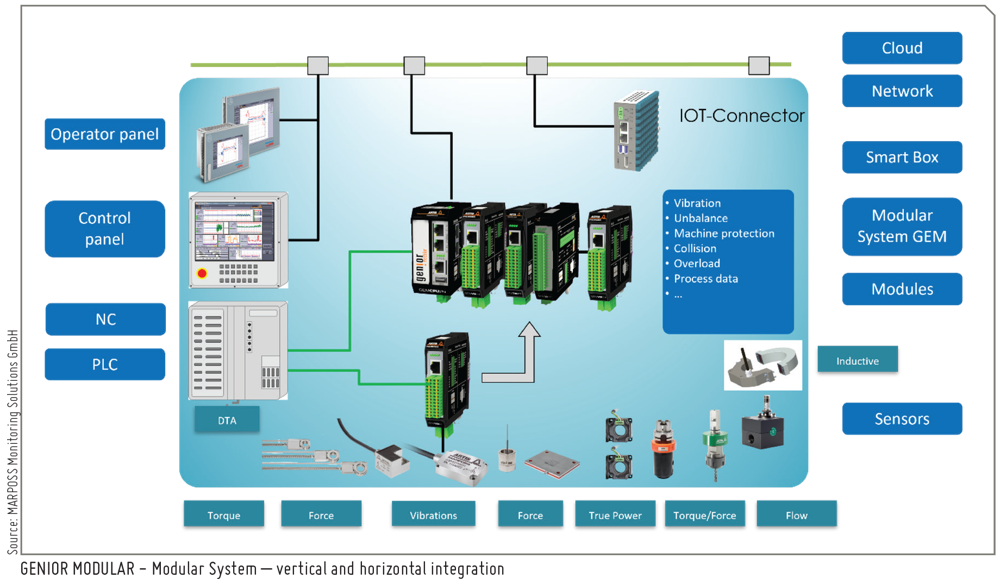
GENIOR MODULAR is a modular system for protecting tools and machines that is installed in the control cabinet. Using self-contained and extremely fast measurement modules, it processes sensor signals in the millisecond range and can communicate directly with the CNC control via fieldbuses such as Profibus, Profinet and EtherNet/IP to receive interface signals for control and, in turn, trigger feed stops, tool changes, or emergency-stop commands.
Vertical integration refers to the alignment of information technology (IT) and operational technology (OT) across different hierarchical levels of a production facility. GENIOR MODULAR achieves this by serving as the data bridge from the raw cutting edge of a machine tool up to executive-level database servers.
Hardware integration is horizontally scalable. On a standard DIN mounting rail, a primary CPU module can be linked to secondary software plug-ins or auxiliary sensor modules using an ‘In-Rail’ CAN-bus connector. This allows a facility to tailor different machines for diverse tasks (e.g., combining collision avoidance with gear hobbing or adaptive control) while using the exact same base architecture.
GEMCMS
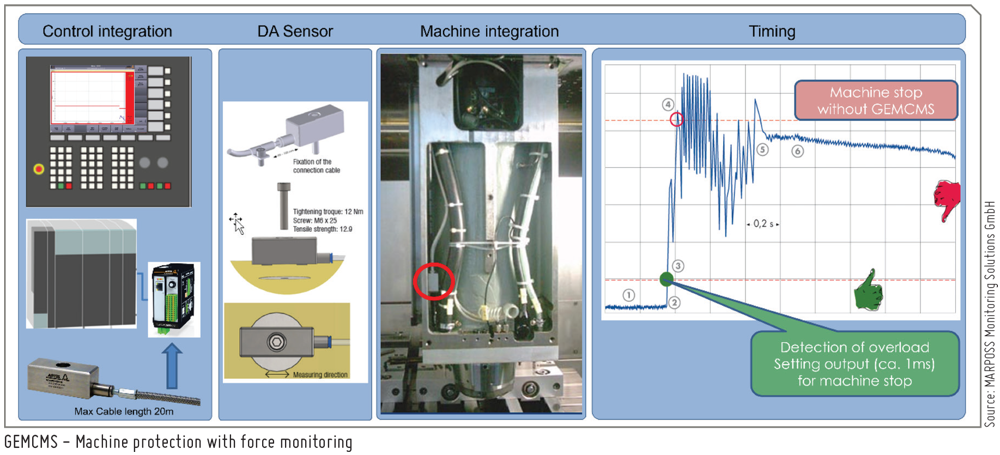
The GEMCMS system from Artis is a highly advanced, self-contained machine protection and collision detection system. It was specifically developed to prevent or reduce costly consequential damage to an absolute minimum caused by programming, setup, or operating errors on machine tools, robots, and handling systems.
The Sensor Matrix: Seamless Detection of All Physical Effects
A machining process emits various physical signals. GENIOR MODULAR stands out because it can simultaneously capture and correlate the entire range of these signals using dedicated sensors and sensor modules.
Active Power Monitoring (True Power)
Measuring the power consumption of spindle and axis motors is a cost-effective method for process monitoring. The Artis systems can either read this data directly in digital form from the CNC bus or capture it as an analogue signal via active power transducers (e.g. control cabinet modules). A tool breakage leads to an abrupt drop in power, while continuous wear causes power consumption to rise slowly.
Torque Monitoring (Digital Torque)
Measuring the torque of spindle and axis motors is usually the most cost-effective method of process monitoring when this data is read directly in digital form from the CNC. A tool breakage typically causes a sudden drop in torque, while continuous wear causes the torque to rise slowly. The advantage of this method lies in its sensorless integration, as the data can be read directly from the NC core, for example via a so-called compile or PLC cycle.
Force and Strain Monitoring
Using strain sensors applied directly to the spindle mount or machine bed, the GENIOR MODULAR measures mechanical deformations in the micrometer range. This enables precise monitoring of feed forces and immediately detects overloads. The technology can be strain gauge- or piezo-based, depending on the required sensitivity and measurement times.
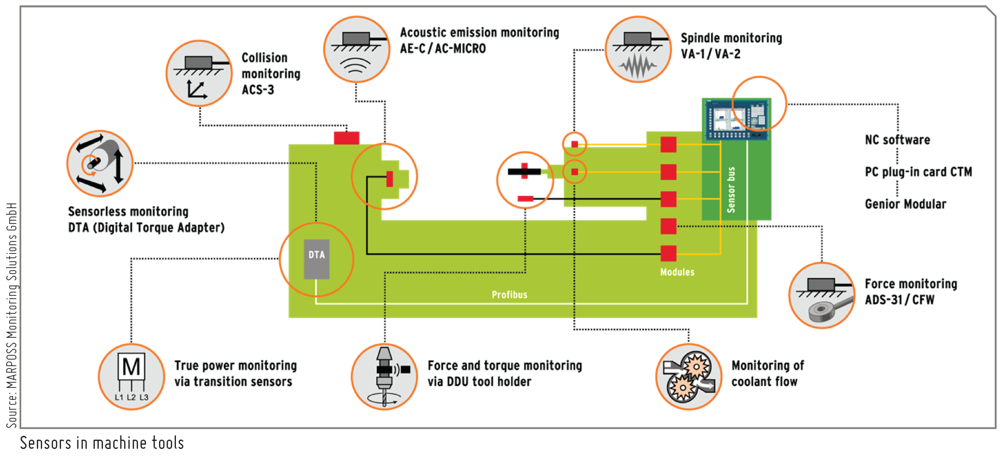
Vibration Monitoring (Vibration/Acceleration)
Piezoelectric or MEMS (micro-electromechanical systems) acceleration sensors monitor the vibration behavior of the spindle. They serve, on the one hand, to detect process-damaging chatter and, on the other hand, as a primary indicator of the spindle’s condition (predictive maintenance). The technology used depends on the required frequency range. MEMS-based sensors are normally cheaper but restricted in the frequency range.
Structural Noise Monitoring (Acoustic Emission – AE)
Structure-borne sound sensors detect high-frequency vibrations in the range of 50 kHz to 400 kHz, which lie far outside the human hearing range. This sensor technology is extremely sensitive and detects micro-cracking of carbide cutting edges milliseconds before the actual fracture, as well as the first physical contact between the tool and the workpiece (cutting-in monitoring). This is essential for very small tools (drills < 1 mm), where the change in active power would be too small for reliable detection.
Process and Collision Monitoring in Autonomous Operation
Real-Time Collision Protection (One-Millisecond Response)
In the event of a collision during rapid traverse (e.g., due to incorrect zero-point offset), milliseconds count. The GEMCMS evaluates the signals from strain or acceleration sensors with an internal cycle time of less than 1 ms. If a defined collision threshold is exceeded, the system triggers a direct hardware interrupt to the drive controller or the emergency stop chain. The drives are actively counter-controlled or de-energized before the kinetic energy can irreparably deform the spindle bearings.
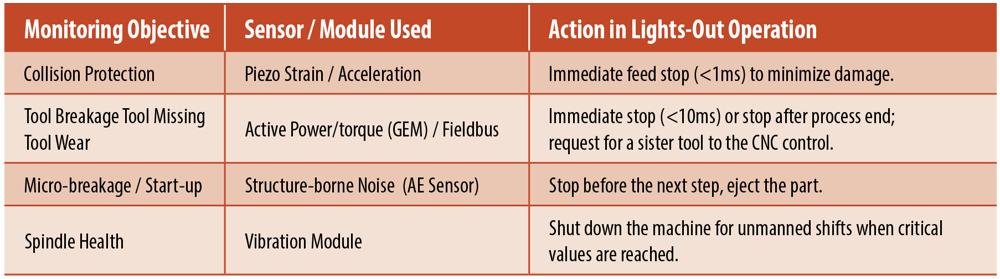
Dynamic Envelope Curve Monitoring in GEM
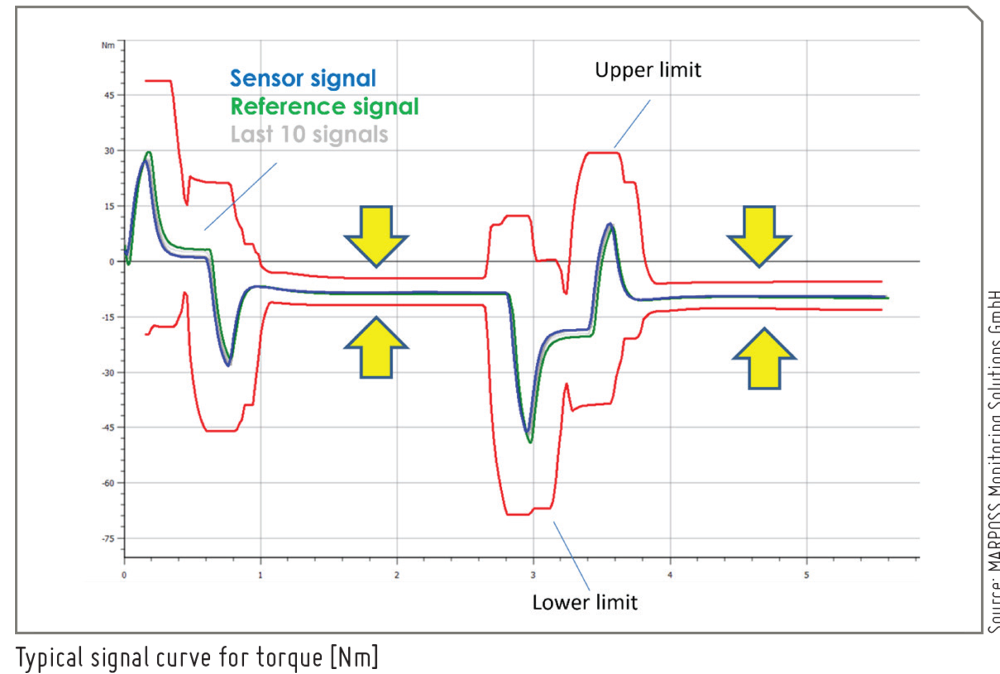
For process monitoring, the system autonomously learns the normal signal curve of a tool during the production of the first good parts (teach-in phase). GEM automatically establishes dynamic envelopes (warning and shutdown thresholds) around this curve.
If the upper warning threshold is exceeded due to increasing wear, GENIOR MODULAR notifies the CNC that the tool must be replaced with a sister tool after completion of the current part. If the shutdown threshold (e.g., in the event of tool breakage) is exceeded, the machine stops immediately to prevent consequential damage. In addition to envelope strategies, a wide range of other algorithms is available to solve almost any monitoring task.
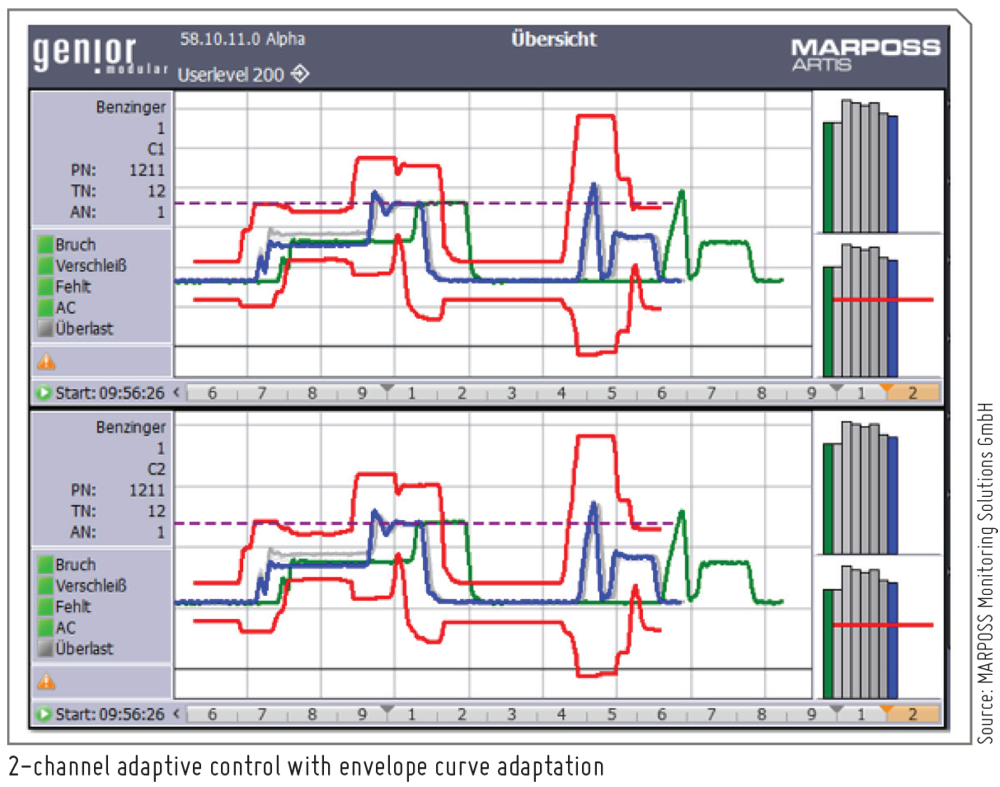 Adaptive Process Control
In machining technology, Adaptive Control (AC) refers to systems that monitor cutting forces and machine conditions in real time. The feed rate is automatically adjusted to the material and tool wear. To prevent the machine from stopping completely when encountering particularly hard areas in the material, MIN defines the absolute minimum value that the feed rate must not fall below at any time in order to avoid tool damage. On the other hand, a MAX value defines the maximum feed rate.
The innovative adaptive control in the GENIOR MODULAR (GEM) allows multiple machining stations to be regulated with regard to idle runs and insufficient or excessive cutting performance, even if they are controlled by a common feed drive. A new feature is the intelligent envelope curve adaptation simultaneously to ensure reliable and sensitive monitoring.
This allows the benefits of an AC system to be combined with optimal tool monitoring. These benefits include compensation for workpiece or material inhomogeneities, tool protection through torque or force control, automatic adjustment for tool wear, increased machining speed while maintaining consistently high quality, and improved process reliability for complex geometries. Some customers have achieved cycle time savings of up to 10 percent.
Condition-Based & Predictive Maintenance in Lights-Out Operation
Before starting an unmanned shift, it must be ensured that the machine can mechanically withstand the hours ahead. GENIOR MODULAR enables condition-based monitoring (CBM):
Spindle climate test / imbalance analysis: An automated test cycle can be run before the shift begins. The system measures the mechanical vibrations of the spindle at various speeds. If the root-mean-square (RMS) values of the vibration increase over time, this indicates incipient bearing damage. The system blocks the machine from running the autonomous shift and issues a warning message.
Business Value & ROIBusiness Value & ROI
The investment in a Marposs Artis GENIOR MODULAR system typically pays for itself within a few months in a lights-out scenario:
- Increased machine uptime: Confidence in the automatic protection system allows for additional unmanned shifts on weekends, which drastically increases OEE.
- Prevention of total losses: The protection of a single motor spindle (often costing between US$ 30,000 and US$ 50,000 plus lost production) fully recoups the cost of the monitoring technology. In the case of expensive tools, such as those used in gear hobbing, costs can quickly run into several thousand euros if faults are detected too late.
- Consistent quality: By detecting process drift and wear in a timely manner, the production of scrap during unmanned operation is effectively reduced to zero.
Conclusion
Lights-out manufacturing poses an incalculable economic risk without intelligent, sensor-based process monitoring. The Artis GENIOR MODULAR system from Marposs, together with the GEMCMS collision monitoring system, provides the technological infrastructure to equip machine tools with the necessary ‘sensory organs’.
 |
Prof Dr-Ing. DIRK LANGE |
 Facebook
.png) Twitter
 Linkedin
 Subscribe